
Best Vacuum Pump for Freeze Dryers: Top Picks for Reliability
Choosing the right vacuum pump and compatible oils is essential for efficient freeze drying. This guide highlights five products that support consistent vacuum performance, extended pump life, and cleaner operation. From oil fluids engineered for direct-drive rotary vane pumps to high-purity synthetic lubricants designed to minimize mist and maintenance, these selections cover oil and pump options that commonly appear in freeze-drying setups.
| Product | Type | Key Benefit |
|---|---|---|
| VacOil ECO Freeze Dryer Vacuum Pump Oil | Vacuum Pump Oil | Molecularly distilled, extends pump life, cools and maintains efficient cycles |
| HCPRO Synthetic Vacuum Pump Oil – Non-Misting | Vacuum Pump Oil | Low volatility, high purity; reduces oil mist and keeps workspace clean |
| HCPRO Synthetic Vacuum Pump Oil – Non-Misting (2) | Vacuum Pump Oil | High purity, non-misting formula; supports longer pump operation |
| HCPRO Synthetic Vacuum Pump Oil – Non-Misting (4) | Vacuum Pump Oil | Same benefits with variation; low vapor pressure for clean environments |
| NAVAC NP7DP Vacuum Pump | Vacuum Pump | Dual-stage, 7 CFM, integrated cooling/valve features for HVAC and refrigeration |
Note: The products listed here focus on pumps and lubricants commonly used with freeze-dryer systems. Always verify compatibility with your specific model and follow manufacturer recommendations for oil types and oil change intervals to maintain optimal vacuum levels.
VacOil ECO Freeze Dryer Vacuum Pump Oil

VacOil ECO Grade is a high-viscosity vacuum pump oil designed for direct-drive rotary vane pumps, ideal for freeze-drying applications. The formula improves pumping cycles, lowers maintenance costs, cools the pump, and extends life. Engineered as a molecularly distilled fluid, it provides robust wear protection and performance advantages compared with other oils. This oil is positioned as the standard choice for oil-sealed rotary vane pumps used in freeze-drying workflows, where consistent vacuum and reduced downtime are critical.
HCPRO Synthetic Vacuum Pump Oil – Non-Misting

This premium synthetic formula emphasizes high purity and low volatility to optimize vacuum efficiency. The non-misting, low vapor pressure design helps maintain a cleaner workspace while supporting rapid evacuation and pump protection. By reducing friction and heat buildup, it contributes to longer pump life and fewer maintenance events, which is valuable for freeze-dryer operations that require reliable cycles and minimal downtime.
HCPRO Synthetic Vacuum Pump Oil – Non-Misting (2)

This variant continues the same core benefits: a high-purity, low-volatility synthetic oil designed to minimize oil mist and support deep vacuum levels. It also aims to extend pump life by lubricating internal components to reduce wear and oxidation. Suitable for freeze-dryer systems that demand sustained performance with fewer oil changes and cleaner operation between runs.
HCPRO Synthetic Vacuum Pump Oil – Non-Misting (4)

This listing mirrors the same high-purity, non-misting, low vapor pressure design. It emphasizes reduced maintenance and extended pump operation, making it suitable for ongoing freeze-drying cycles where consistent vacuum is essential for product quality and process efficiency.
NAVAC NP7DP Vacuum Pump

The NP7DP is a Pro Series vacuum pump featuring a dual-stage AC motor, a 7 CFM flow rate, and integrated oil circulation. It includes a check valve to maintain vacuum if power is interrupted, and an oil mist filter to trap excess mist, promoting a cleaner work area and stable vacuum. It is designed for HVAC and refrigeration applications but is widely used in laboratory and freeze-dryer setups that require reliable, continuous vacuum performance.
NAVAC NP7DP Vacuum Pump – (2)
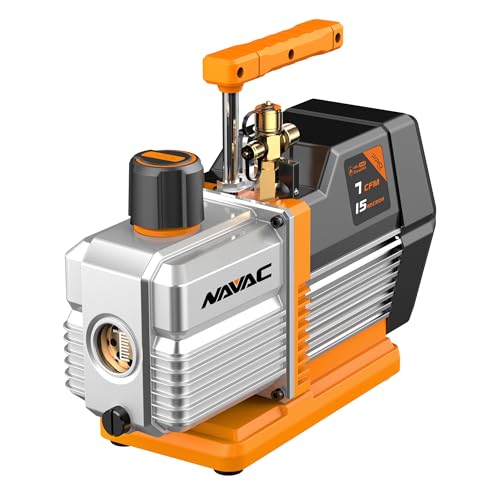
This listing presents a variant of the NAVAC NP7DP with similar dual-stage capabilities and integrated oil circulation. Features include a check valve to prevent backflow and an oil mist filter for cleaner operation. It remains suitable for freeze-dryer workflows that demand steady vacuum levels across multiple cycles and running conditions.
Buying Guide: Key Purchase Considerations
When selecting a vacuum pump or oil for freeze-drying, consider the following perspectives to balance performance, cost, and long-term maintenance.
- Vacuum performance and application fit: For freeze drying, aim for pumps with ample CFM, reliable deep vacuum capability, and compatibility with direct-drive rotary vane systems. Dual-stage configurations can improve efficiency and achieve lower ultimate vacuum.
- Oil type and maintenance: Oil choice affects pump life, oil mist generation, and cleanliness of the workspace. Synthetic, non-misting oils with low vapor pressure reduce maintenance and improve longevity, especially in tight or cleanroom-like environments.
- Contamination control: Oil mist filters and check valves help prevent oil carryover and backflow, preserving system integrity and reducing post-run cleanup.
- Compatibility and lifecycle costs: While premium oils and pumps may have higher upfront costs, they often reduce downtime, extend service life, and lower total cost of ownership over time.
- Noise, heat, and cooling: Consider pumps with efficient cooling and noise levels suitable for your lab or facility. Proper cooling systems prevent heat buildup that can impact vacuum efficiency.
- Future proofing: If you plan to expand capacity or run longer freeze-drying cycles, choose pumps with scalable flow rates and robust seals designed for repetitive use.
- Brand and support: Reputable brands with readily available replacement parts and oil options simplify maintenance and ensure consistent performance.
For optimal results, match the pump’s specifications to your freeze-dryer model recommendations, and maintain a regular oil-change schedule aligned with manufacturer guidelines. Store oils and lubricants in a clean, temperature-controlled area to preserve viscosity and performance.